What We Can Manufacture
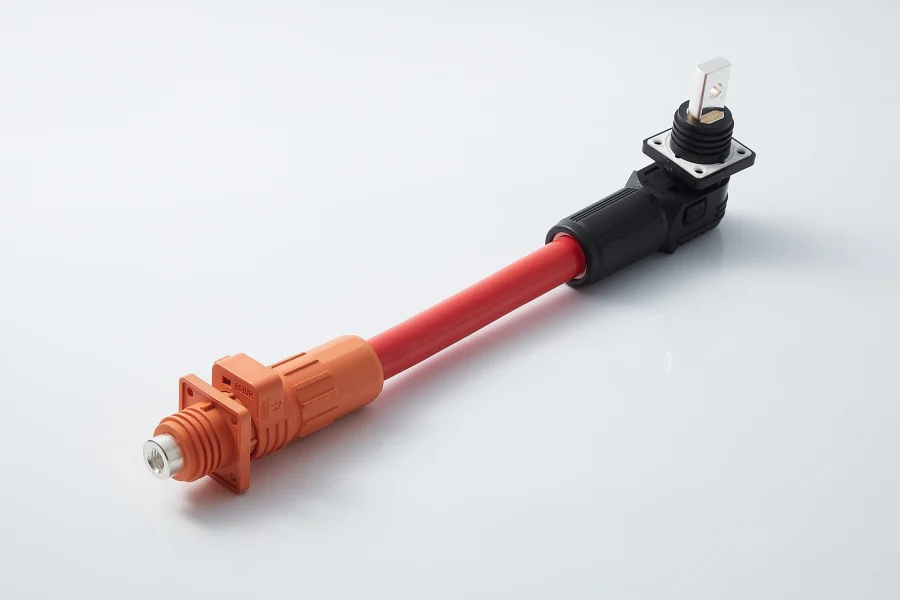
Connectors
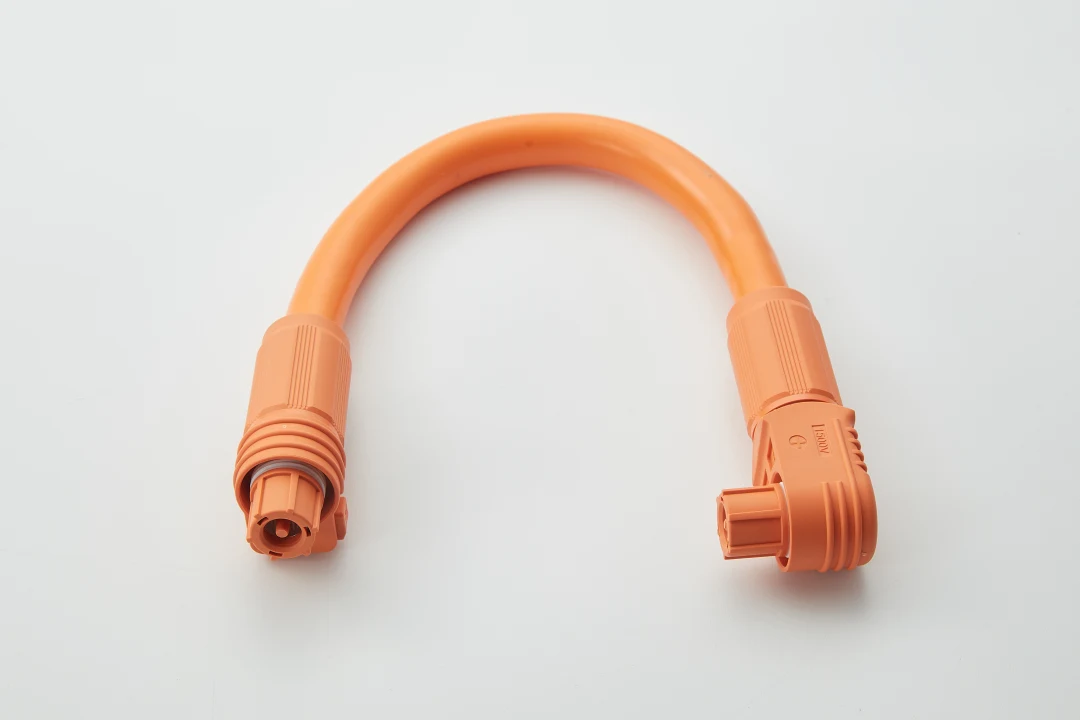
We supply battery connectors as individual parts or together with the finished wire harness or cable assembly. We review the mating connector, mounting arrangement and termination requirements to identify a configuration for your equipment.
CN battery connector series — Model-dependent options from 70 to 500 A and up to 1500 VDC.
View the CN Connector Series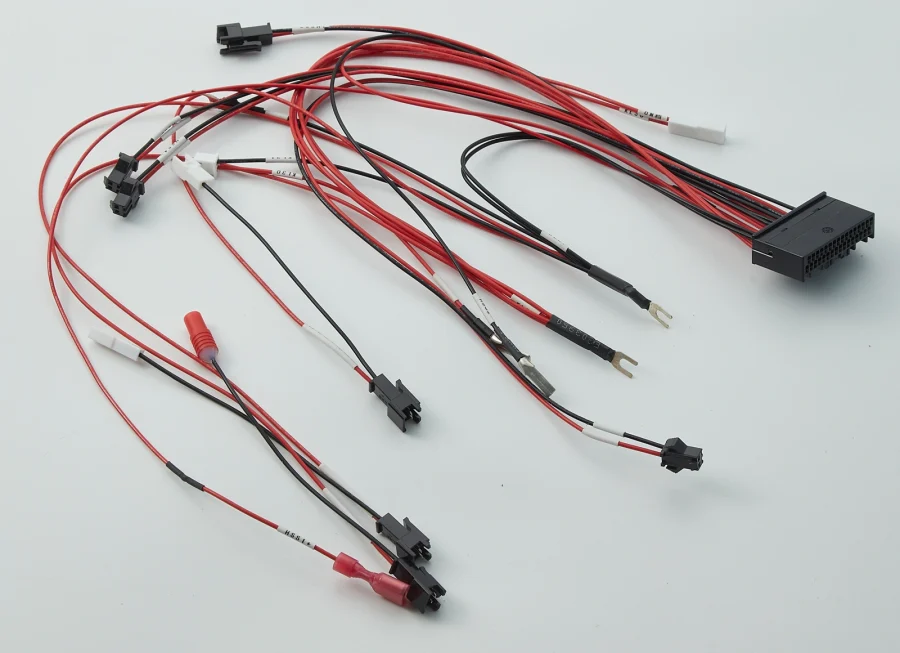
Wire Harnesses
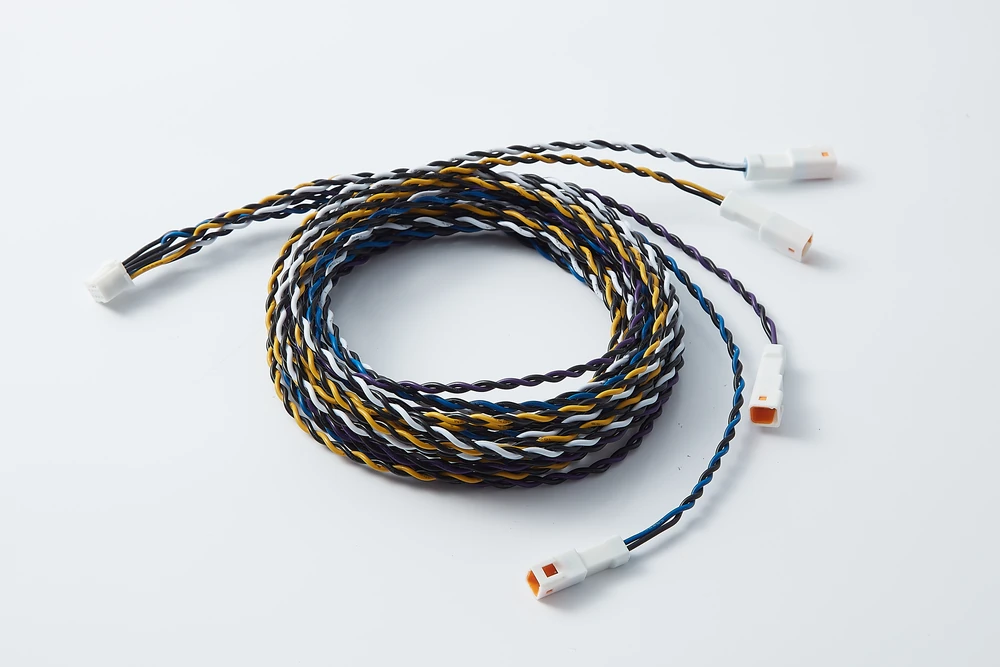
We build harnesses with multiple connectors, circuits and branches. The approved pinout and layout define where each wire terminates, where branches leave the main bundle and where sleeves, labels or other protective parts are fitted.
Example — BMS acquisition harnesses with multiple sensing leads and defined connector positions.
View BMS Acquisition Harnesses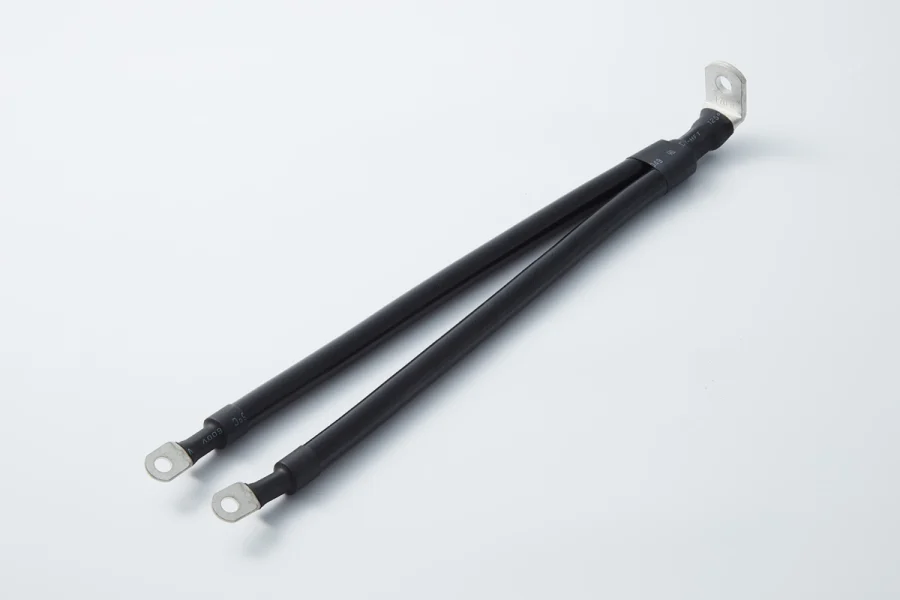
Cable Assemblies
We build terminated cable assemblies with connector, ring-terminal and other specified end combinations. We confirm the termination at each end, the finished length, the exit direction and any heat-shrink covering or molded cable exit required for the build.
Battery cable options — 6 AWG to 4/0 AWG or 10 to 185 mm², depending on the cable and termination combination.
View Battery Cable AssembliesHow to Start Your Project
Have a Drawing or BOM?
For build-to-print projects, send your current drawing, BOM, wiring diagram or pinout. We review the revision, specified part numbers, order quantity and what the finished product needs to include. If you are open to alternate parts, we can review available options against the mating interface and project requirements. Any proposed change goes to you for approval before use.
Send Drawings or BOMHave a Sample or Application Requirement?
A physical sample, clear photos or details of the equipment connection can start the review. We use what you share to identify the mating parts, mounting constraints and dimensions that still need to be confirmed. We then discuss whether an existing series can meet the requirement and whether a proposed modification or tooling needs further review.
Discuss a SampleFrom Project Review to Production
-
Project Review
We review your drawing, BOM or sample to confirm what we’ll supply. We identify missing dimensions, conflicting part numbers and inspection requirements that still need to be agreed.
-
Quotation & Sampling
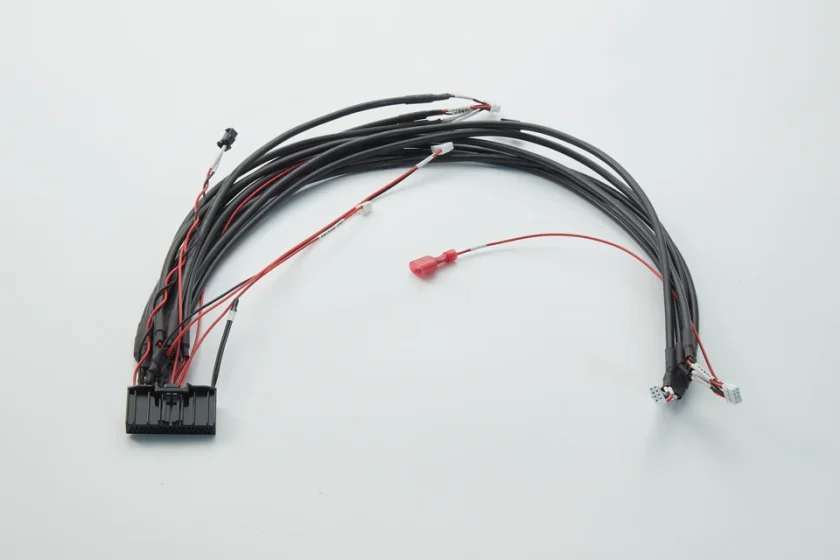
We confirm what the quote covers, how many samples you need and the proposed schedule. If the build requires a mold or fixture, we cover the tooling arrangements in the quote.
-
Sample Approval
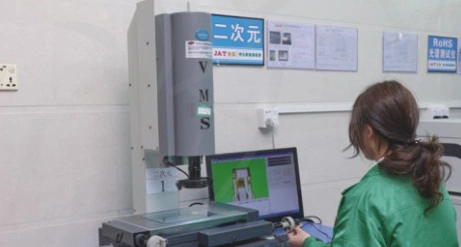
If your project includes sampling, you check fit, cable reach, routing and agreed inspection items. We record approved changes and confirm the production revision and any agreed first-article documentation.
-
Production & Delivery
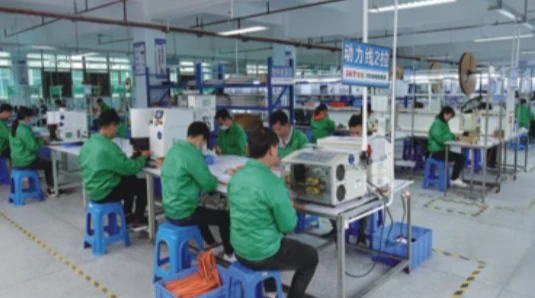
We build to the approved revision, carry out agreed inspections and pack to order requirements, including labels and lot identification. Before repeat production, we confirm the applicable revision and any approved changes.
Manufacturing at JTY
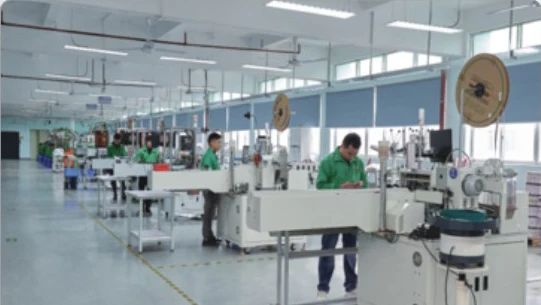
Connector Supply & Assembly
We supply battery connectors for customers who assemble their own equipment, and we also supply finished assemblies with those connectors fitted. At our assembly stations, crimped contacts are inserted into housings to build connector-ended leads and harnesses.
For a project that needs both the connector and the finished assembly, we review the two together so the specified connector, contacts and cable are carried through to the build.
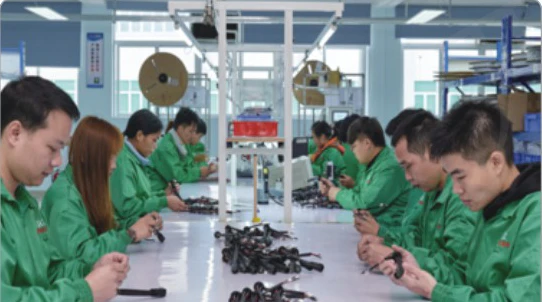
Wire Harness Manufacturing
Our workshop uses automatic terminal machines and operator-run stations for wire-end processing and crimping. At the assembly benches, terminated wires are fitted into their specified housing positions and brought together into the finished harness.
On a branched build, the team assembles each group of wires to its connection end and fits the specified sleeves, protective coverings and identification labels. The completed harness brings the main bundle, branches and connectors together in the layout approved for the equipment.
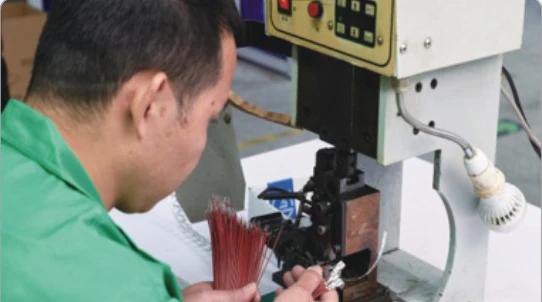
Cable Termination
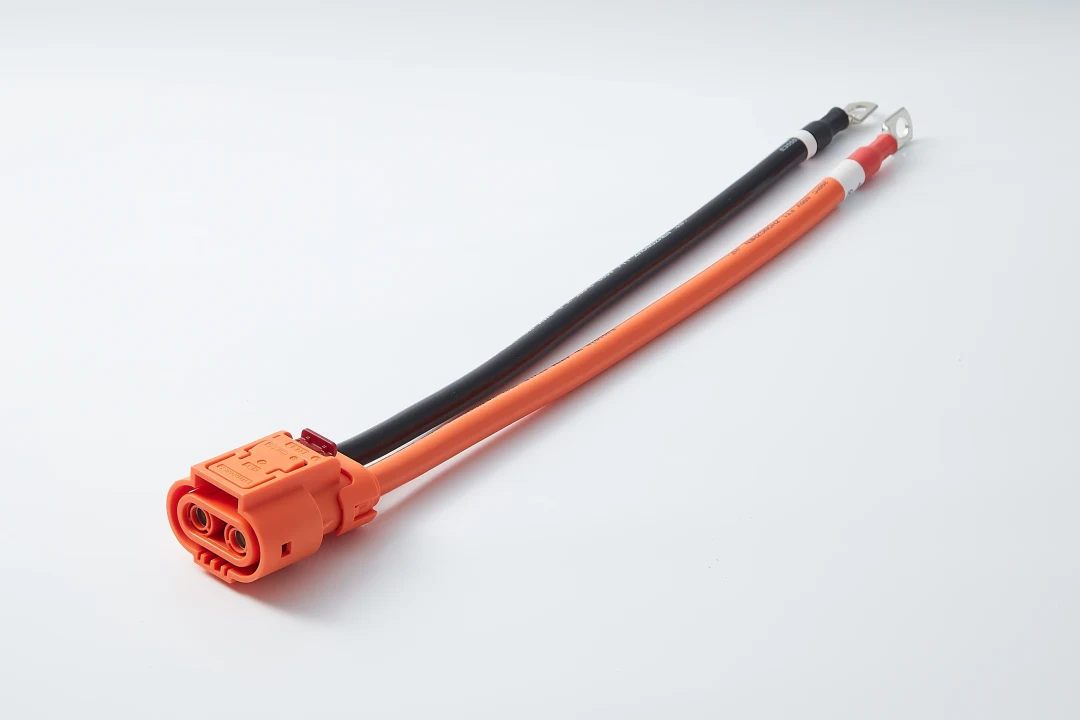
Our cable assembly work includes connector-to-ring-terminal and ring-to-ring builds. At the termination stations, we fit the specified connector contact or lug to each cable end.
Where the drawing calls for heat-shrink covering, we apply it at the specified termination. The finished lead is built with the two end fittings, length and exit orientation defined for the equipment.
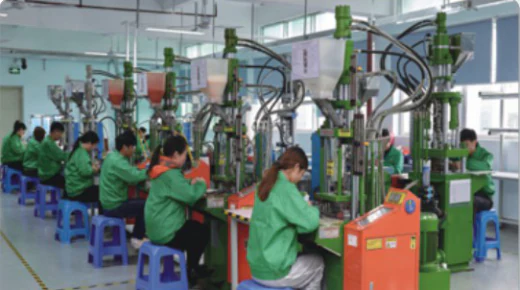
Vertical Overmolding
For molded-end products such as circular connector leads, we use vertical injection molding equipment to form the cable exit around the terminated assembly.
The molded profile, cable diameter and exit direction are part of the agreed construction. This lets us build the finished end to the shape and orientation specified for the installation.

Quality & Inspection at JTY
We check crimped terminations and finished assemblies against the approved drawing and the test limits agreed for your build.
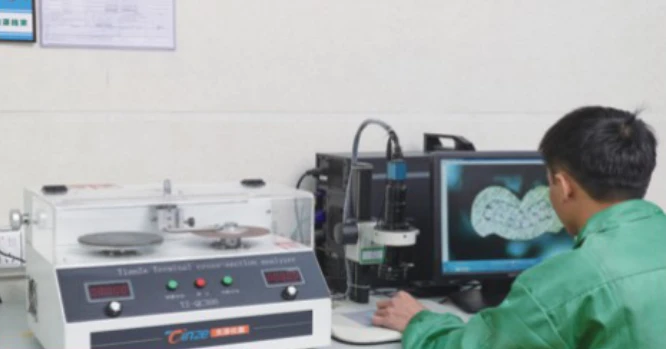
In-Process Termination Checks
We examine crimp cross-sections for conductor compression and insulation grip. We compare measured crimp dimensions with the agreed requirements for the terminal and wire. First samples with crimped terminations include a crimp cross-section report.
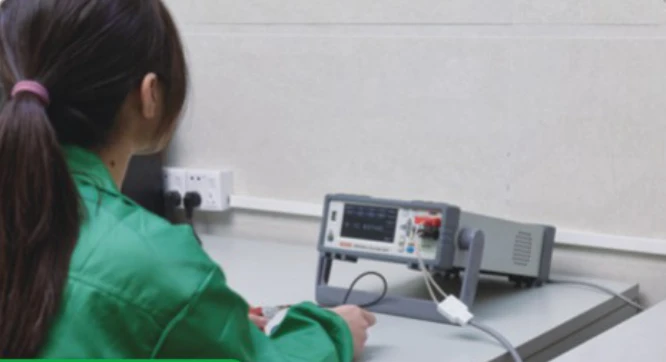
Finished Assembly Inspection
We check cable length, branch lengths and molded-end dimensions against the approved drawing where applicable. We can verify continuity, polarity and pin assignment against the wiring diagram and measure circuit resistance against the specified limit.
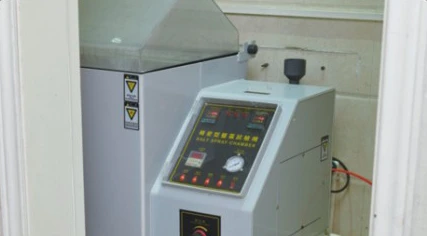
Project-Specific Testing
Depending on the application, we can run dielectric withstand, temperature rise, connector mating force, cable flex or salt-spray tests. We agree the test conditions and acceptance criteria with you for the specific assembly.
Custom Manufacturing FAQs
Can we start with just a physical sample or photos?
Yes. Send clear photos of both ends and, for a harness, the full layout. Tell us what the part connects to and what needs to stay the same. We can start the review from photos and let you know if we need the physical sample to confirm dimensions, mating fit or wiring before quoting.
Can JTY modify an existing connector series?
We first check whether a configuration in the existing series meets your mating, mounting and termination requirements. If you need a change, send the current part number and explain what must change. We review feasibility and confirm whether a new sample or tooling is needed.
How are sample quantities, MOQs and lead times determined?
Sample quantity depends on what you need to approve. The minimum batch order depends on the build and its components. Samples typically take 3–7 days once the configuration is agreed, and batch production takes about 30 days after order confirmation. We confirm quantities and timing in your quote.
How do you handle changes on repeat orders?
We confirm the drawing revision and approved components before repeat production. If a drawing or part changes, we review the effect on fit, wiring and inspection with you. We confirm whether a new sample or revised inspection is needed before building to the new revision.
Can you use a specified connector brand or an approved equivalent?
Send the brand and exact part number if your BOM requires an original connector. We check availability and quote to the specified BOM. If you allow alternatives, we can review a cross-reference against the mating interface and electrical requirements and use it after your approval.
Can we arrange an NDA before sharing drawings or sending a sample?
Tell us if you need an NDA before sending proprietary files. Share a non-confidential project summary and the NDA terms for review first. If you plan to send a physical sample, contact us first to confirm shipping details and what to include.
Contact Us
Tell JTY about your connector, wire harness or cable assembly project. Share the drawings, specifications or sample details you have for an initial review.
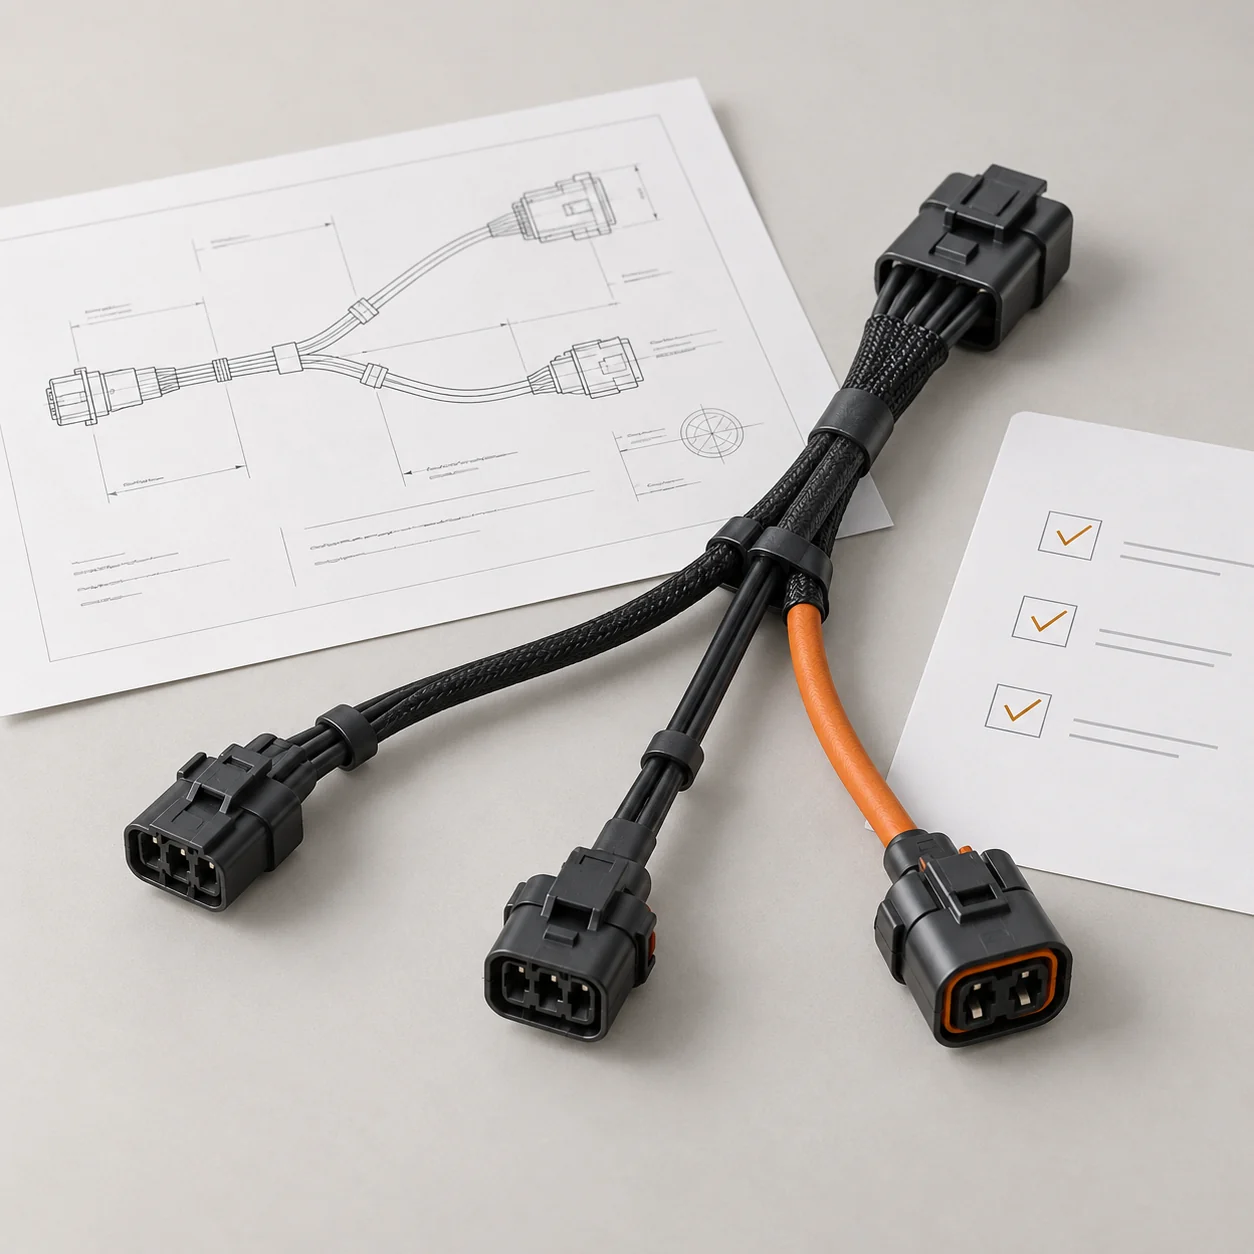 Your Project